Integrating a Packaging Machine into an Existing Production Line

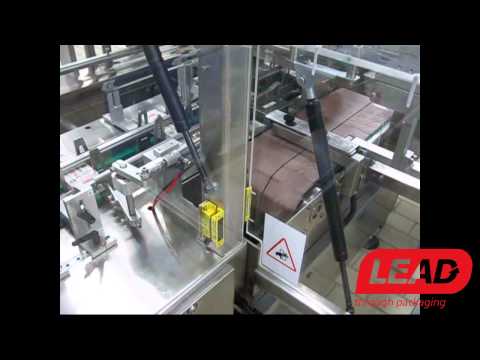
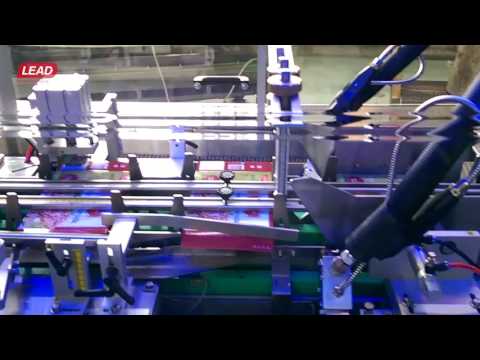
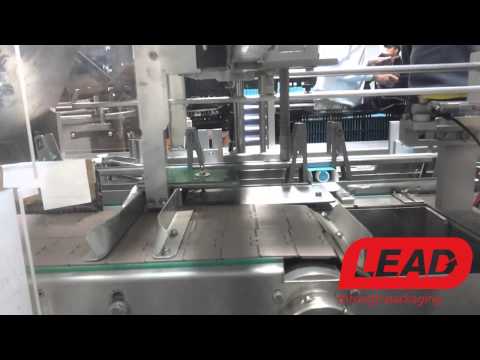
Purchasing a new machine for an existing production line is fundamentally different from building a new line. The existing line sets requirements such as conveyor heights, production rates, distances, and control interfaces, and the new machine must be integrated with them while keeping production downtime to a minimum. A packaging machine can be suitable for the product and still create a bottleneck if its interfaces with the existing line are not evaluated in advance. This article focuses on the practical checks that should be carried out before the machine is ordered, rather than relying only on catalog specifications.

What Should Be Checked on Site Before Ordering?

The site assessment should be completed before the machine specification is finalized. These details are easy to overlook, but any of them can affect the proposed solution and its cost.

  • The conveyor height at the machine’s infeed and discharge, compared with the height of adjacent stations 
  • Available floor space, including sufficient access for servicing, cleaning, and movement around the machine 
  • The route for moving the machine into the factory, including door and opening widths, ceiling height, and available lifting points
  • Available site infrastructure, including electrical power, compressed air, and drainage where required 
  • Product flow direction, to ensure that the machine does not require the product flow to be reversed

It is also important to map operator movement around the existing line. A machine installed in an area used for carts or operator movement can create an operational problem that is not obvious from the layout drawing. Layout planning should therefore be part of the initial assessment, rather than something addressed afterward.

How Should the New Machine’s Throughput Be Matched to the Existing Line?

The overall line throughput is limited by its slowest stage. Installing a faster machine after a slower station will not necessarily increase throughput. Instead, the new machine may remain idle while it waits for products from the preceding station. The first question should therefore be how much product the existing line can actually supply, rather than the new machine’s maximum speed.

The new machine should therefore be evaluated against the actual feed rate rather than its catalog-rated speed. When assessing an existing production line, the relevant figure is not the maximum rate of the preceding machine, but the rate it actually delivers during routine operation, including short stops and slowdowns. The difference between the two can be significant.

In practice, a small difference in rates can often be managed with an intermediate conveyor buffer, which absorbs short-term fluctuations and helps the machine operate continuously. Larger gaps require a different solution, such as upgrading the slower station or choosing a model that matches the existing rate. The MP-50 sleeve binder can operate at up to 120 sleeves per minute, but that capacity is relevant only if the preceding loading station can supply product at a comparable rate.

How Is the New Machine Integrated with the Existing Control System?

A stand-alone machine can operate through its own control panel. A machine integrated into a production line needs to communicate with the other equipment. It may need to stop when the downstream station is blocked, report faults to the existing control system, and, in some configurations, receive product recipes from a central controller instead of requiring the operator to enter them manually. The required level of integration varies between facilities, so it should be defined in the specification rather than left to the installation stage.

Machines designed for line integration need to provide appropriate communication interfaces in addition to their local control panels. On a production line with several stations operating in sequence, transferring the product recipe from a central controller can eliminate repeated data entry and help maintain consistent settings between stations. This can be particularly useful when the same product is produced on several lines simultaneously.

It is also worth considering how easily the machine can be adapted to future changes. The MKH-4 cartoner’s feeding system can be separated in one second, allowing changes to the feeding arrangement without modifying the main machine body. This type of design can simplify future line modifications and reduce the work required to adapt the machine.

How Can Installation Downtime Be Minimized?

Installation downtime depends on the scope of the line modification rather than simply on the size of the machine, so there is no standard duration. What can be controlled is how the installation work is prepared and sequenced. The more preparation that can be completed while the line is still operating, the shorter the required downtime window is likely to be.

Electrical preparation, conveyor adjustments outside the active installation area, and machine testing without product should be completed before the shutdown whenever possible, reducing the amount of work required during the available downtime.

Interface pointWhat needs to be checked?Potential issue if overlooked
Conveyor heightCompatibility with nearby stationsConveyors may need to be modified during installation
Feed rateActual output of the preceding stationThe machine may operate below its available capacity
Area and accessSpace for service and cleaningMaintenance may become more difficult and time-consuming
Control interfaceStopping, fault reporting, and recipe transferThe operator may need to operate two control systems separately
Machine access routeOpening widths and ceiling heightDelivery may be delayed or require non-standard lifting arrangements

What Role Does Engineering Design Play in Line Integration?

Integrating a packaging machine into an existing line is where a standard catalog solution may not be sufficient. IMPAC handles the design, manufacture, and full integration of production lines, so the assessment begins by mapping the entire line rather than focusing on a single machine. This approach allows the machine interfaces to be adapted to the existing factory conditions rather than requiring the production area to be redesigned around the machine.

The measurements should also be documented rather than relying only on memory or photographs. A simple drawing showing the line layout, heights, distances, and product flow direction can shorten the assessment process and allow the supplier to evaluate feasibility before the site visit. If the line has changed over time, older drawings may no longer reflect the current layout, making a new site measurement necessary.

What Should Be Considered When Integrating a Complete Packaging Line?

When an integration involves multiple machines, the number of interface points and coordination requirements also increases. A fully automated packaging line can move products through multiple packaging stages without manual handling between stages. This means that each stage depends on the performance of the preceding stage. Inconsistent feeding can cause a cartoner to stop, while an uneven product flow to a sleeve binder can affect the consistency of the packaging process.

A complete line also requires decisions about where buffers are needed. An intermediate buffer between stations can absorb short-term fluctuations and help machines operate more continuously, but it also requires space and adds another point to the material flow. The line assessment should determine where a buffer is needed and where it can be omitted, based on the expected variation at each stage.

A machine being added to an existing line therefore needs to be evaluated for both product requirements and line compatibility. These two considerations can lead to different machine choices. If they are considered separately, compatibility issues may not become apparent until installation.

It is also important to define in advance which supplier is responsible for each part of the interface. Connecting a new machine to existing equipment may involve two suppliers. Without a clear division of technical responsibility, issues can be passed between the parties while the line is out of operation. Clearly documenting these responsibilities in the specification can help avoid delays during installation and commissioning.

Summary

Successful integration of a packaging machine depends not only on the machine specifications but also on how well it fits the existing line interfaces. Conveyor height, feed rate, available access space, and control interfaces are among the key factors that influence the complexity of an installation.

Contact IMPAC’s engineering team to arrange a line survey and interface assessment before finalizing the machine specifications.
Questions and Answers

How Can a New Machine Be Integrated While Minimizing Production Downtime?

Some preparation can be completed while the line is running, such as preparing the required infrastructure and making conveyor adjustments outside the machine installation area. The connection itself and start-up should be carried out during a planned stop. Completing as much preparation as possible in advance can help shorten the required downtime.

What Happens if the New Machine Is Faster Than the Existing Line?

It will operate at the rate at which the existing line can supply product, rather than at its maximum rated speed. Small differences in rates can often be managed with an intermediate buffer, while larger differences may require upgrading the slower station or choosing a different machine model.

What Information Is Needed for the Line Assessment?

A drawing or measurements of the existing line, conveyor heights, the operating rates of nearby stations, and a list of the formats that run through the line can all be useful. This information can shorten the assessment process and help identify potential installation issues in advance.

Does the Machine Need to Be Connected to the Factory Control System?

It depends on the required level of integration. In a synchronized line, the machine may need to exchange status and fault signals with adjacent stations and stop when required by the line controls. In a simpler configuration, it may operate as an independent station through its own control panel.
More articles

Videos

Search product ▼
All products
Automatic line for bundling yogurt cups in carton packaging
Automatic system for packing frozen meat products in cartons
Automatic line for filling and closing tahini buckets
FLEXEO-P Semi-Automatic IBC Filling and Capping Machine
Automatic system for packing ice cream products in cartons for Fromageries (Pronery)
Automatic system for packing products in cartons for Almandos
Automatic line for filling and capping 25-liter jerry cans
Automatic system for filling and closing containers for Sonol
MKH-3 - Envelopes
TL-01 TRAY ERECTOR
CW-01 Case Packer for Wrap Around Carton Packaging.
MP-50 Continuous Sleeve Bundling Packaging Machine
FD-68
Continuous Horizontal Cartoner (MKH-4)
Carton Tray Packaging Machine (TP-01)
Sleeve Bundler (70-MP)
Continuous Sleeve Bundler (10-MP)
Pick & Place (PK-01)
Machine for closing supplies
FLOWPACK
Cup in special packaging – four-pack
Cup in special packaging – pair
Bottles
Small bottles
Yogurt in a sleeve
Cup – pack of four
Cup – pair
Master carton + side Load
Top Load – top feeding
Master carton side Load
Master carton Top Load
Filling and packaging project
Carton setup and top feeding
Master carton with triple feeding
Pick and place for trays
Tray setup and top feeding
Master carton wrap around
PYTHON - Automatic inline machine for filling and packaging jars
Semi-automatic machine for filling granules by weight
Automatic rotary machine for filling and sealing cups
Liquid filling with pipette sealing
Bottle filling and capping
High-speed bottles (PACKER)
Filling bulk products and packaging them in a bag
Horizontal packaging machine
Aseptic liquid filling in bags
Weighing and filling machine for powders and granules
Automatic line for filling and closing jerrycans
Automatic machine for filling jerrycans at high speed (200 per minute) (PACKER)
Automatic machine for filling buckets at high speed (PACKER)
Semi-automatic filling machine
Automatic for filling drums
Semi-automatic machine for filling cubes and barrels
Packaging fresh cheese cubes in cardboard trays
Tray packer – 2-tier feeding
Tray packer – side feeding
Tray forming with top feeding + stacker
Filling and setting up a tray + side feeding
Tray packer – side feeding
Setting up a box and filling dates
Machines for packaging bottles into cartons
Packaging cream cheese in carton boxes
Honeycomb tray setup
Horizontal Cartoner (MKH-3)
Tuck-in
Frozen food
Ice bag
Ice cream packaging machine
Vertical machine – Flip Top – gum and candies
Toys – box
Box for balls
Carton packaging for tobacco
12 bags of 100g in a box
Packaging up to 120 per minute
Packaging up to 30 per minute
Packaging a long product
Hanging for boxes – Tuck-in
Tissue packaging
2 products in a box
Packaging cans in a box at a speed of 180 per minute
Pick and place – packaging plastic clamshell containers into carton boxes
Pick and place – packaging vacuum coffee bags into RSC cartons
Continuous machine with manual feeding
Feeding cups into a box
Case wrap around
Special yogurt pair
Yogurt in two levels
Tuna – pack of four
Carton packaging for tuna cans – pack of four
Soft can packaging
Packaging cans in groups of three
Partial carton sleeve
Tray packaging into sleeve
Glass bottles
Single cup

Automatic line for bundling yogurt cups in carton packaging

Automatic line for bundling yogurt cups in carton packaging

Automatic system for packing frozen meat products in cartons

Automatic system for packing frozen meat products in cartons

Automatic line for filling and closing tahini buckets

Automatic line for filling and closing tahini buckets

FLEXEO-P Semi-Automatic IBC Filling and Capping Machine

FLEXEO-P Semi-Automatic IBC Filling and Capping Machine

Automatic system for packing ice cream products in cartons for Fromageries (Pronery)

Automatic system for packing ice cream products in cartons for Fromageries (Pronery)

Automatic system for packing products in cartons for Almandos

Automatic system for packing products in cartons for Almandos

Automatic line for filling and capping 25-liter jerry cans

Automatic line for filling and capping 25-liter jerry cans

Automatic system for filling and closing containers for Sonol

Automatic system for filling and closing containers for Sonol

MKH-3 - Envelopes

MKH-3 - Envelopes

TL-01 TRAY ERECTOR

TL-01 TRAY ERECTOR

CW-01 Case Packer for Wrap Around Carton Packaging.

CW-01 Case Packer for Wrap Around Carton Packaging.

MP-50 Continuous Sleeve Bundling Packaging Machine

MP-50 Continuous Sleeve Bundling Packaging Machine

FD-68

FD-68

Continuous Horizontal Cartoner (MKH-4)

Continuous Horizontal Cartoner (MKH-4)

Carton Tray Packaging Machine (TP-01)

Carton Tray Packaging Machine (TP-01)

Sleeve Bundler (70-MP)

Sleeve Bundler (70-MP)

Continuous Sleeve Bundler (10-MP)

Continuous Sleeve Bundler (10-MP)

Pick & Place (PK-01)

Pick & Place (PK-01)

Machine for closing supplies

Machine for closing supplies

FLOWPACK

FLOWPACK

Cup in special packaging – four-pack

Cup in special packaging – four-pack

Cup in special packaging – pair

Cup in special packaging – pair

Bottles

Bottles

Small bottles

Small bottles

Yogurt in a sleeve

Yogurt in a sleeve

Cup – pack of four

Cup – pack of four

Cup – pair

Cup – pair

Master carton + side Load

Master carton + side Load

Top Load – top feeding

Top Load – top feeding

Master carton side Load

Master carton side Load

Master carton Top Load

Master carton Top Load

Master carton Top Load

Master carton Top Load

Filling and packaging project

Filling and packaging project

Carton setup and top feeding

Carton setup and top feeding

Master carton with triple feeding

Master carton with triple feeding

Pick and place for trays

Pick and place for trays

Tray setup and top feeding

Tray setup and top feeding

Master carton wrap around

Master carton wrap around

PYTHON - Automatic inline machine for filling and packaging jars

PYTHON - Automatic inline machine for filling and packaging jars

Semi-automatic machine for filling granules by weight

Semi-automatic machine for filling granules by weight

Automatic rotary machine for filling and sealing cups

Automatic rotary machine for filling and sealing cups

Liquid filling with pipette sealing

Liquid filling with pipette sealing

Bottle filling and capping

Bottle filling and capping

High-speed bottles (PACKER)

High-speed bottles (PACKER)

Filling bulk products and packaging them in a bag

Filling bulk products and packaging them in a bag

Horizontal packaging machine

Horizontal packaging machine

Aseptic liquid filling in bags

Aseptic liquid filling in bags

Weighing and filling machine for powders and granules

Weighing and filling machine for powders and granules

Automatic line for filling and closing jerrycans

Automatic line for filling and closing jerrycans

Automatic machine for filling jerrycans at high speed (200 per minute) (PACKER)

Automatic machine for filling jerrycans at high speed (200 per minute) (PACKER)

Automatic machine for filling buckets at high speed (PACKER)

Automatic machine for filling buckets at high speed (PACKER)

Semi-automatic filling machine

Semi-automatic filling machine

Automatic for filling drums

Automatic for filling drums

Semi-automatic machine for filling cubes and barrels

Semi-automatic machine for filling cubes and barrels

Packaging fresh cheese cubes in cardboard trays

Packaging fresh cheese cubes in cardboard trays

Tray packer – 2-tier feeding

Tray packer – 2-tier feeding

Tray packer – side feeding

Tray packer – side feeding

Tray forming with top feeding + stacker

Tray forming with top feeding + stacker

Filling and setting up a tray + side feeding

Filling and setting up a tray + side feeding

Tray packer – side feeding

Tray packer – side feeding

Setting up a box and filling dates

Setting up a box and filling dates

Machines for packaging bottles into cartons

Machines for packaging bottles into cartons

Packaging cream cheese in carton boxes

Packaging cream cheese in carton boxes

Honeycomb tray setup

Honeycomb tray setup

Horizontal Cartoner (MKH-3)

Horizontal Cartoner (MKH-3)

Tuck-in

Tuck-in

Frozen food

Frozen food

Ice bag

Ice bag

Ice cream packaging machine

Ice cream packaging machine

Vertical machine – Flip Top – gum and candies

Vertical machine – Flip Top – gum and candies

Toys – box

Toys – box

Box for balls

Box for balls

Carton packaging for tobacco

Carton packaging for tobacco

12 bags of 100g in a box

12 bags of 100g in a box

Packaging up to 120 per minute

Packaging up to 120 per minute

Packaging up to 30 per minute

Packaging up to 30 per minute

Packaging a long product

Packaging a long product

Hanging for boxes – Tuck-in

Hanging for boxes – Tuck-in

Tissue packaging

Tissue packaging

2 products in a box

2 products in a box

Packaging cans in a box at a speed of 180 per minute

Packaging cans in a box at a speed of 180 per minute

Pick and place – packaging plastic clamshell containers into carton boxes

Pick and place – packaging plastic clamshell containers into carton boxes

Pick and place – packaging vacuum coffee bags into RSC cartons

Pick and place – packaging vacuum coffee bags into RSC cartons

Continuous machine with manual feeding

Continuous machine with manual feeding

Feeding cups into a box

Feeding cups into a box

Case wrap around

Case wrap around

Special yogurt pair

Special yogurt pair

Yogurt in two levels

Yogurt in two levels

Tuna – pack of four

Tuna – pack of four

Carton packaging for tuna cans – pack of four

Carton packaging for tuna cans – pack of four

Soft can packaging

Soft can packaging

Packaging cans in groups of three

Packaging cans in groups of three

Partial carton sleeve

Partial carton sleeve

Tray packaging into sleeve

Tray packaging into sleeve

Glass bottles

Glass bottles

Single cup

Single cup

No results found