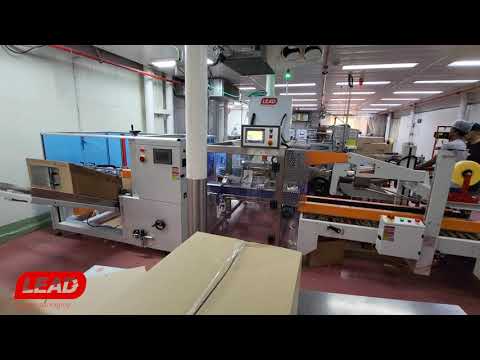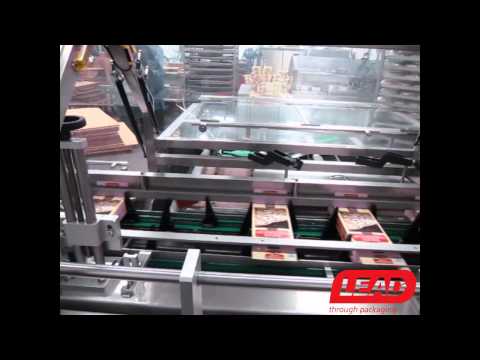
The downtime of a packaging machine is measured not only in the minutes during which the machine is idle, but also in the product that accumulates in front of it and the orders that leave the plant late. In facilities where packaging is the final stage before shipment, a 30-minute stoppage can affect everything that follows. Preventive maintenance shifts maintenance from a reactive response to a planned part of the production schedule, making it possible to schedule work instead of carrying it out during an unplanned shutdown.

What is the difference between preventive maintenance and breakdown maintenance?
Breakdown maintenance begins when something goes wrong. It includes the time needed to diagnose the problem, wait for repairs, and restart the machine. Preventive maintenance, by contrast, is carried out according to a planned schedule, at a predetermined time when the machine is available and safe to service. The main difference does not necessarily lie in the scope of the work, but in when the work is performed and whether the timing is planned.
Planned maintenance also makes it possible to perform several tasks during the same scheduled shutdown. Wear inspection, cleaning, calibration, and checking spare parts inventory levels can be carried out together instead of causing four separate stoppages over the course of a month. A well-planned maintenance program can therefore reduce both the number of stoppages and the time spent handling them.
Which components of packaging machines require regular maintenance?
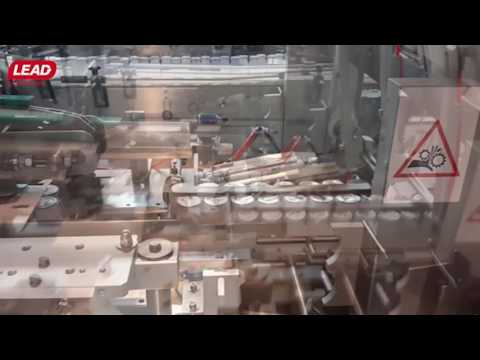
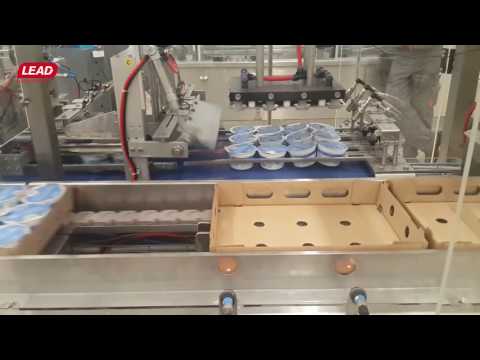
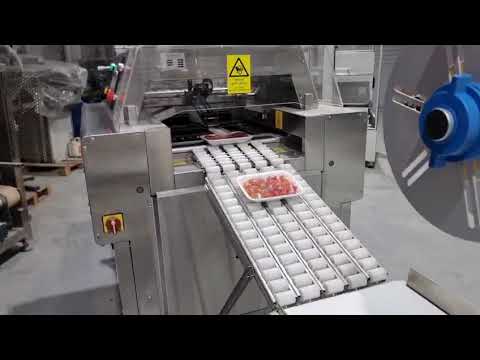
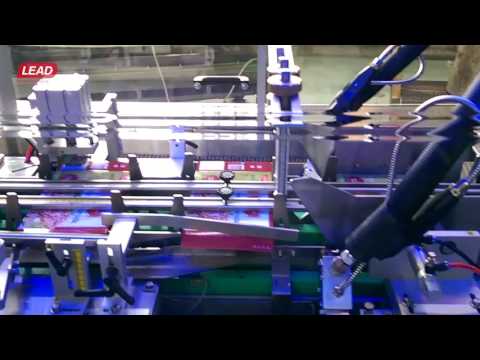
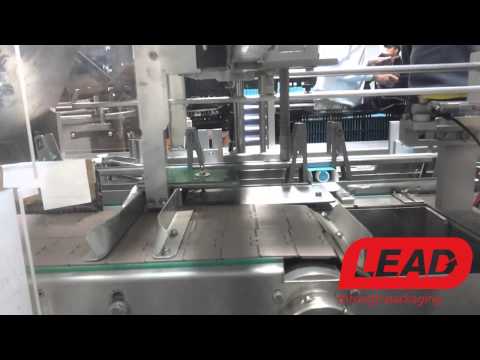
Wear usually occurs in machine components of packaging equipment that are exposed to repeated contact, heat, or rapid movement. These include material feeding mechanisms, gripping elements at the loading station, belts and conveyors, as well as cutting and folding components in machines operating from web material.
These components should be included in the maintenance plan and monitored regularly.
▪ Mechanisms for feeding and separating sheets of packaging material
▪ Gripping and holding elements for the product at the loading station
▪ Conveyor belts, bearings, and drive wheels
▪ Cutting and folding components in machines operating from web material
▪ Sensors and photoelectric cells that can be affected by contamination
In practice, some faults that appear to be mechanical may actually be caused by contamination. Cardboard residue, product dust, and accumulated oil can interfere with sensor readings and cause the machine to stop even when there is no actual mechanical failure. Regular cleaning should therefore be treated as part of routine maintenance, not as a separate task.
How should maintenance be planned in relation to production?
The maintenance program works better when it is coordinated with the production schedule. A practical approach is to plan maintenance when the line is already stopped anyway, for example during format changes, cleaning between products, at the end of a shift, or on a no-production day. A short maintenance task performed during a format change can eliminate the need for a separate technical stoppage, whereas the same task performed in the middle of a production cycle may require additional downtime.
The intervals between maintenance inspections should be based on the manufacturer’s instructions and the machine’s actual operating hours, not on the general calendar. A machine running one shift per day and a machine running three shifts may reach the same number of cycles at very different rates. A schedule based solely on calendar dates can therefore lead to servicing one machine too early and another too late.
How should you determine which spare parts to keep in stock?
An effective spare parts inventory does not need to be large. It should focus on components whose absence could significantly affect production. The important factor is not only the component’s price, but what will happen if it is not available.
A low-cost component whose absence could stop the line for a week may be more important to keep in stock than an expensive component for which a temporary replacement is available. That is why it is worth classifying components by expected lead time and by the impact their absence may have on production, rather than solely by catalog classification.
| Action | When to perform | What problems does it help prevent? |
| Cleaning sensors and product paths | Every time you change the format or clean the machine | False stops and feeding faults |
| Wear tests of gripping elements | Based on cumulative operating hours | Product damage and incorrect packaging |
| Inspection of belts and conveyors for stretch and wear | During planned downtime | Slippage, product misalignment, and line stoppage |
| Calibration after component replacement | Immediately after completing the replacement | Packaging the entire batch with deviations |
| Checking critical spare parts inventory | Regularly | Long replacement lead times during failures |
In addition to maintaining stock, it is worth documenting every maintenance task and every failure. After a few months, these records can show which components repeatedly require intervention and help determine whether the problem is due to normal wear or to setup and operating conditions.
How does machine design affect maintenance requirements?
Maintenance requirements are partly influenced by the machine’s design and the accessibility of its components. A machine that provides good service access, enables quick disconnection of feeding elements, and allows cleaning without unnecessary disassembly can reduce the time required for routine maintenance throughout its service life. The MKH-4 cartoner feeding system can be disassembled in one second, which shows how fast access to machine components can affect routine maintenance time. Impac designs and manufactures its machines in-house, which means accessibility and cleaning requirements can be taken into account already at the machine specification stage, rather than only after installation.
How does preventive maintenance fit into an automated packaging line?
In an automated packaging line, downtime at one station can stop the entire sequence, making unplanned stoppages more disruptive than in a standalone machine. For this reason, maintenance should be planned at the line level, not for each machine separately. Maintenance tasks for several stations can be combined within the same planned shutdown, and priority can be given to stations that do not have a bypass. A station affecting the carton in the middle of the sequence has a different priority than a station that can be temporarily bypassed.
Automated packaging machines can also provide useful operational data, including cycle counts, downtime, and recurring faults. Even without an advanced monitoring system, recording this data at the end of each shift can provide a numerical basis for determining maintenance intervals, rather than relying solely on the crew’s assessment.
The transition from reacting to breakdowns to planned maintenance does not happen overnight. A practical approach is to start with the station that causes the longest line stoppages, develop a maintenance plan for it, and then extend that approach to the other stations. This allows you to measure the results early, before the same approach is applied to other stations.
What is the operator’s role in the maintenance program?
Some actions that help prevent downtime do not require a technician. Cleaning at the end of the shift, visual inspection of belts and gripping zones, and reporting unusual noises or movements can be part of the operator’s daily work. These observations can be useful because operators work with the machine for longer periods and may notice changes before they develop into a failure.
For this to work, there must be a clear person or process for reporting problems, and the reports must be documented. A short end-of-shift checklist with space for comments can turn operators’ observations into useful service data. Without documentation, the same fault may keep recurring without being properly resolved.
Key takeaways on packaging machine maintenance
Reducing downtime starts with moving from reactive maintenance to planned maintenance: identifying wear-prone components, scheduling maintenance work around existing stoppage points, setting intervals based on actual operating hours, and systematically documenting maintenance activities. A well-designed preventive maintenance program can help reduce both the number of stoppages and the time spent resolving them, and machines designed with good service accessibility can make routine maintenance easier. Contact the Impac engineering team to discuss at the machine specification stage which solutions for access, disassembly, and cleaning are suitable for your production requirements.